Thermoforming film guide
PA/PE vs PA/EVOH/PE Thermoforming Films: Which Structure Fits Your Food Pack?
Both structures have a clear role. The right structure depends on the product, forming depth, lidding film, MAP need, storage condition, and shelf-life target.
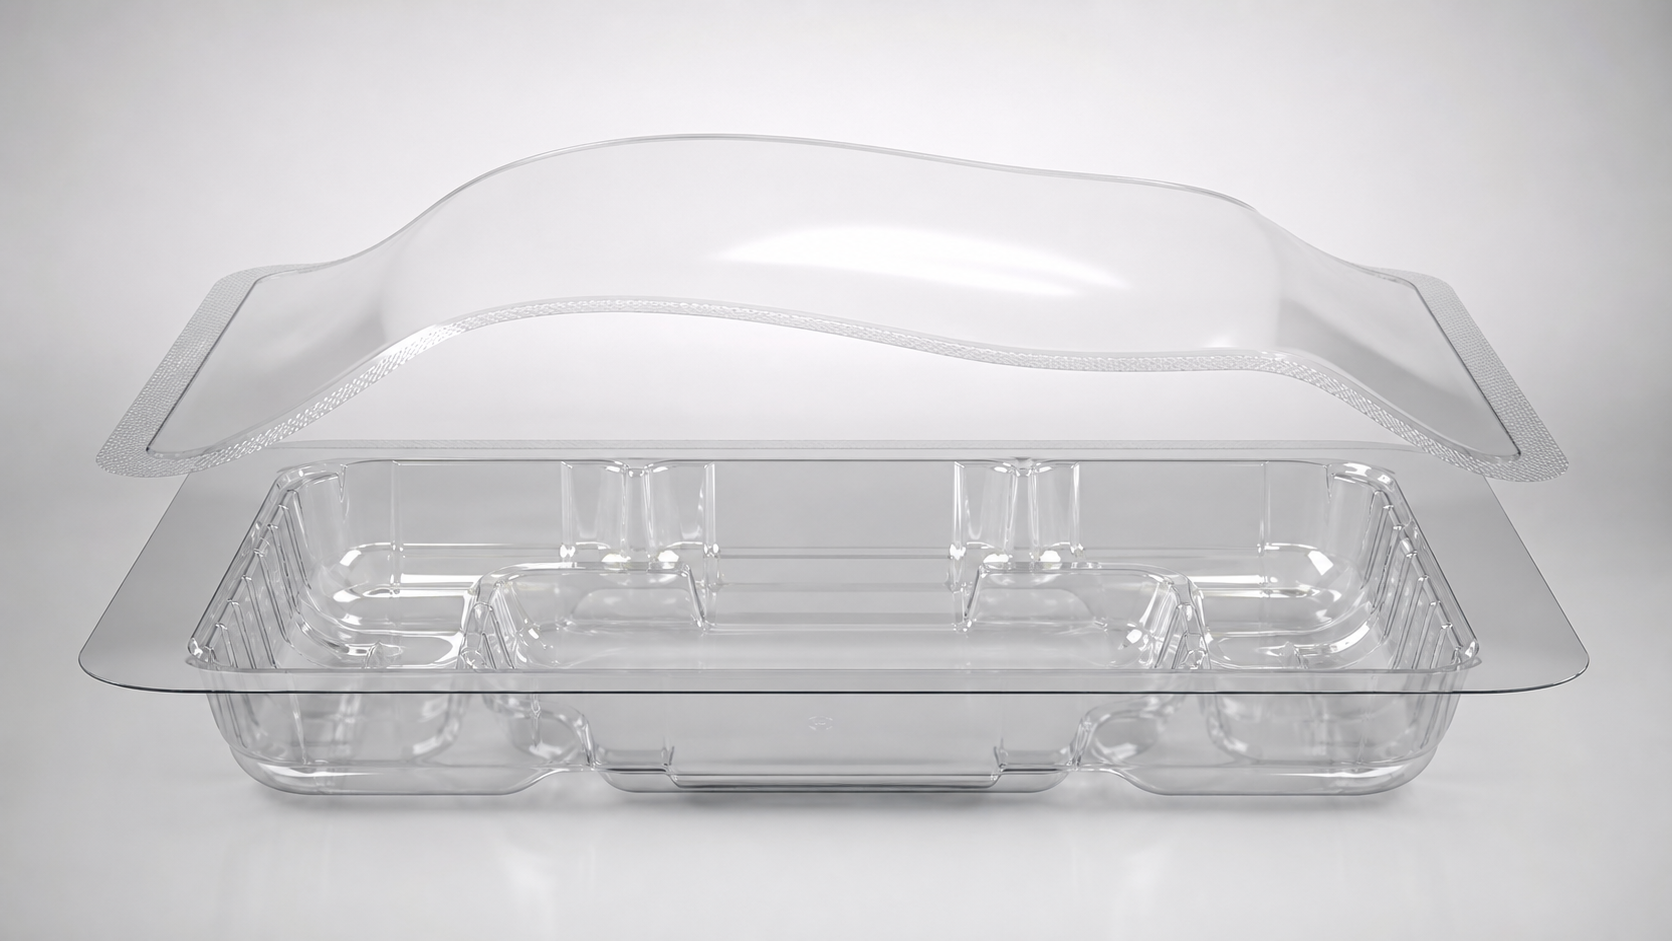
When a buyer asks for flexible thermoforming film, the structure choice often starts with two families.
PA/PE.
PA/EVOH/PE.
Both have a place in coextruded forming-film structures. But they are not selected for the same reason.
What PA does in a thermoforming film
PA, or polyamide, is commonly used in forming-film structures because it helps with toughness, puncture resistance, and forming performance.
In a bottom web, that matters because the film is not staying flat. It is heated, stretched, and formed into a cavity. After forming, it still has to carry the product, resist handling stress, and protect weak points around the cavity.
PA/PE: practical standard barrier structure
PA/PE is usually the first structure for clear flexible thermoforming packs where toughness, formability, and seal reliability are the main priorities.
- Clean forming
- Good puncture resistance
- Clear presentation
- Reliable sealing to a compatible top web
- Practical performance for chilled food packs
PA/PE does not mean one fixed film. Thickness, layer design, PE sealant choice, forming behavior, and top-web compatibility still need to match the pack.
PA/EVOH/PE: high barrier structure
PA/EVOH/PE adds the EVOH barrier layer into the structure. This becomes important when oxygen control is central to the pack.
In MAP packaging, the film, lidding film, seal, gas mix, and storage plan all work together. If the product is oxygen-sensitive, or if the shelf-life target is stricter, a high-barrier structure may be needed.
- Oxygen sensitivity
- Shelf-life extension
- Export movement
- MAP gas retention
- Product quality over chilled storage
Why the lidding film matters
The bottom film cannot be selected in isolation.
The lidding film decides how the seal behaves. It also affects peel or weld performance, pack appearance, MAP retention, and the final consumer experience.
- Top-web structure
- Sealant compatibility
- Peel seal or weld seal need
- Seal temperature and dwell time
- Pack contamination risk near the seal area
Do not decide only by micron
Thickness matters, but it is not the full answer.
A 100 micron film from one structure may not behave the same as a 100 micron film from another structure. The forming depth, layer design, resin selection, and machine recipe can change the result.
Where each structure tends to fit
Choose PA/PE when the main need is a clear, tough, sealable forming film for food packs where standard barrier performance is acceptable.
Review PA/EVOH/PE when oxygen control becomes part of the shelf-life strategy, especially for MAP packs or export-linked applications.
What to send for a faster recommendation
- Product name and packed weight
- Pack size and cavity depth
- Current bottom-film thickness
- Existing structure, if known
- Lidding film or top-web details
- Machine format and bottom-web width
- MAP gas mix or vacuum need
- Storage condition and shelf-life target
- Current issue on the line or in distribution
Final thought
PA/PE and PA/EVOH/PE are both practical flexible thermoforming film directions. The difference is not only technical. It is commercial too.
PA/PE is the standard barrier structure when toughness, formability, clarity, and sealing are the priority.
PA/EVOH/PE is the high-barrier structure when oxygen control and shelf life are more central to the pack.
Nexus Corporation supplies 5 and 7 layer flexible coextruded PA/PE and PA/EVOH/PE thermoforming bottom films in 50 to 250 microns.
Send the product, cavity, lidding film, storage condition, and shelf-life target.
Request structure input